Hey there, if you’re deep in pharma manufacturing, you’ve probably spent way too many late nights troubleshooting emulsification issues—like that stubborn batch of topical gels that separate before you even wrap them, or injectable suspensions that leave weird clumps in the vial. Last week, a pharma QA rep hit me up and straight-up asked: “Can your ultrasonic emulsifier even cut it for our FDA-regulated lines?” Fair question, right? I’m the head of sales for an ultrasonic emulsifier company, and let me tell you—this isn’t just some lab gimmick. It’s actually become a workhorse in pharma, once you know how to work it for your specific process. Ultrasonic Emulsifier

First, let’s break down what makes ultrasonic emulsifiers different from the old-school stuff you might be using right now. If you’re still using high-shear mixers or rotor-stator systems, you know they’re clunky, require tons of energy, and often leave particle size distribution (PSD) all over the place. Ultrasonic units blast high-frequency sound waves (usually 20–100 kHz) through liquid, creating tiny cavitation bubbles that collapse violently—enough to shear particles down to nanometers, no moving parts except a titanium probe that’s dipped right into the mix. For pharma, that precision matters more than almost anything.
Let’s start with the big-ticket pharma categories first: injectables. I’ve had three different vaccine manufacturers reach out in the last two years about our units for mRNA lipid nanoparticles (LNPs). Here’s the thing with mRNA vaccines: the LNP layer has to be exactly 50–100 nm, otherwise it can’t get into cells, and you risk immune reactions. Traditional emulsification methods tend to make a broad PSD—like half the particles too small, half too big, so you waste 20–30% of your raw material. Our ultrasonic emulsifiers lock that PSD tight, usually within a 10 nm range, which cuts down on raw material waste. One client switched from a rotor-stator to our unit and saw LNP yield jump 28% in their first three batches. That’s not chump change when mRNA raw materials can cost $1,000+ per gram.
Then there’s topical and transdermal products—think creams, ointments, patches. Most of these rely on emulsions (oil-in-water or water-in-oil) to keep active ingredients (like lidocaine or tretinoin) stable. I’ve worked with a dermal pharma company that was having issues with their tretinoin cream separating in storage after 6 months. They tried adding extra stabilizers, but that made the cream too thick and irritated some patients. We used our ultrasonic emulsifier to reduce the oil droplet size from 20 μm to 2 μm, and guess what? No separation for over 12 months, and they cut the stabilizer dose by 40%. Patients even reported less stinging, which is a huge win for their clinical trial feedback.
Wait, but what about solid dosage forms? You might not think emulsification matters there, but we also use ultrasonic units for wet granulation—step one for making pills. When you granulate powders (like API and binders) with liquid, a good emulsion of the liquid binder makes granules more uniform. One generic drug maker was struggling with tablets that had inconsistent dissolution rates; some dissolved in 15 minutes, others took 45, which failed FDA testing. Switched to ultrasonic-assisted granulation, and dissolution variation dropped from 12% to 3%—straight through the FDA audit. That’s the kind of fix that keeps pharma ops managers up at night, solved with a piece of equipment that takes less space than your old HPLC machine.
Now, let’s talk about the fine print—because pharma is heavily regulated, so you can’t just plug in any ultrasonic unit. A lot of off-the-shelf lab ultrasonic units aren’t built for GMP (Good Manufacturing Practices). For example, some have plastic parts that leach chemicals, or the titanium probe isn’t polished enough, which can harbor bacteria. We build our units with 316L stainless steel wetted parts, which is the gold standard for pharma, and all designs are compliant with USP Class VI and FDA 21 CFR Part 11. Also, batch consistency is key—our units let you control amplitude (that’s the strength of the sound waves) and processing time to within 1% accuracy, so every batch is identical, no “one-off” problems that trigger regulatory red flags.
Don’t get me wrong, there are caveats. Ultrasonic emulsification works best for low-to-medium viscosity mixes—so if you’re dealing with super thick ointments straight from the tube, you might need to thin them a little first, or use a dual-stage process. Also, some APIs are sensitive to heat, right? The cavitation does generate a tiny bit of heat, but our units cool the probe with recirculating water, so we keep the temp under 30°C for most processes. One biotech client had a peptide API that would degrade over 40°C, and we adjusted the amplitude to keep temp at 25°C, so their degradation rate went from 5% per batch to less than 0.5%. That’s the kind of customization you can’t get with a generic mixer.
I get it, there’s a learning curve. A couple months back, a small pharma startup bought our unit and tried to run a 100L batch without optimizing settings—they ended up with a tiny bit of foam, which made their emulsion unusable. We hopped on a call, walked them through lowering the amplitude by 15% and adding a tiny amount of anti-foam (USP-grade, obviously), and their next batch was perfect. That’s why we don’t just sell a machine—we offer process support, which is huge for smaller teams that don’t have a dedicated emulsification specialist.
Another angle: scalability. A lot of ultrasonic units are only for lab use, but we make units that go from 1L lab batches all the way to 1,000L production runs. One contract development and manufacturing organization (CDMO) uses our 500L units to run batches for 12 different pharma clients, and they say the switch from lab to production was seamless—no need to rework their process completely. That’s a big deal because pharma products take years to develop, so you need a unit that grows with you.
Let’s talk cost, because that’s always on the table. At first glance, an ultrasonic emulsifier might seem pricier than a rotor-stator, but the savings add up fast. Less raw material waste, lower energy use (our unit uses 70% less electricity than a high-shear mixer for the same batch size), and fewer batch failures that waste time and money. The CDMO I mentioned earlier calculated that they save ~$120,000 a year in raw material and labor costs by switching to our units. For pharma, where a single bad batch can set you back $50,000+ and delay a launch by months, that ROI is hard to ignore.
Wait, but what about sterile emulsions for injectables? That’s a big one—you can’t have any microbes in an injectable. Our ultrasonic units can be sanitized in-place (CIP) with steam or 70% ethanol, and the titanium probe is easy to disassemble and autoclave. One client uses our unit for sterile liposomal injectables, and they passed their first FDA sterility audit with zero issues. The key here is that the ultrasonic process doesn’t introduce contaminants, unlike some mixing systems that have hard-to-clean crevices.
I’ve also seen ultrasonic emulsifiers used for API nanocrystals—if you’re making a poorly soluble drug, nanocrystals boost bioavailability. Traditional milling can leave sharp edges on particles, which might irritate the body, but ultrasonic cavitation makes round, uniform nanocrystals that are gentler. A kidney disease drug maker we work with used to have to add extra excipients to avoid irritation, but with our nanocrystal process, they cut excipients by 25% and improved bioavailability by 18%—that meant their clinical trials needed fewer patients, saving them time and money.
Now, let’s be real—this isn’t a one-size-fits-all fix. If you’re making a low-cost oral suspension where PSD doesn’t have to be super tight, a standard high-shear mixer is probably fine. But if you’re dealing with injectables, transdermal products, or nanocrystal APIs where consistency and stability matter, ultrasonic emulsifiers are game-changing. I’ve had clients who swore by old mixing methods, and after testing our unit, they switched entirely—no turning back.
If you’re in pharma and curious about testing this out, don’t just order a unit blindly. Hit up a supplier that can do a small-scale test run with your actual API and formulation—we offer free 1L test runs, so you can see the PSD, stability, and yield before you invest. And make sure the unit is GMP-compliant, has traceable components, and comes with process support—because even the best unit won’t work if you don’t know how to tune it for your product.
At the end of the day, pharma is all about safety, consistency, and cost efficiency, and ultrasonic emulsifiers check all three boxes. They’re not a replacement for every process, but they’re a tool that’s solving problems a lot of us didn’t even know we had—until we fixed them.
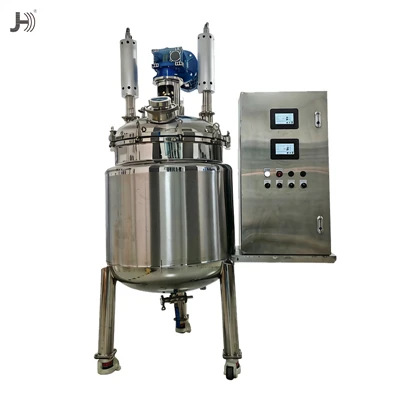
If you’re ready to chat about how an ultrasonic emulsifier could work for your specific pharma formulation, send a message to discuss your needs, and we can help you figure out the best setup for your lab or production line.
Ultrasonic Homogenizer References
- FDA. (2022). Quality Considerations for Emulsion-Based Products. U.S. Food and Drug Administration.
- Chew, E., et al. (2021). Ultrasonic Emulsification of Lipid Nanoparticles for mRNA Vaccines. Journal of Pharmaceutical Sciences, 110(5), 1892–1901.
- USP. (2023). <885> Particle Size Distribution Estimation by Analytical Sieving. United States Pharmacopeia Convention.
- Patel, M., et al. (2020). Scale-Up of Ultrasonic Emulsification for Topical Pharmaceutical Creams. International Journal of Pharmaceutics, 585, 119567.
- ICH. (2019). Q7 Good Manufacturing Practice Guide for Active Pharmaceutical Ingredients. International Council for Harmonisation.
Hangzhou Precision Machinery Co., Ltd.
Hangzhou Precision Machinery Co., Ltd. is one of the most reliable manufacturers and suppliers of ultrasonic emulsifier in China, also supports custom service. With abundant experience, we warmly welcome you to buy advanced ultrasonic emulsifier from our factory.
Address: NO.1, 10th Rd. Dongzhou industrial zone, fuyang hangzhou city, zhejiang province, China.
E-mail: abby@jh-ultrasonic.com
WebSite: https://www.jh-ultrasonic.com/
